In the UFS R&D department, extensive testing was carried out using different tool types and configurations. The development process began with super-high-speed steel (HSS) tap materials and progressively introduced other metals to identify higher-performance alloys.
The objective was to develop a solution capable of combining high productivity, extended tool life and reliable tapping performance when machining medium- to high-strength steels.
The target materials include carbon steels, alloy steels and stainless steels, including work-hardening, austenitic and ferritic grades.
HSSV3 and a specialized geometry
The research identified HSSV3, a high-speed steel containing 3% vanadium, as the optimal material for the V82 and V83 tap series.
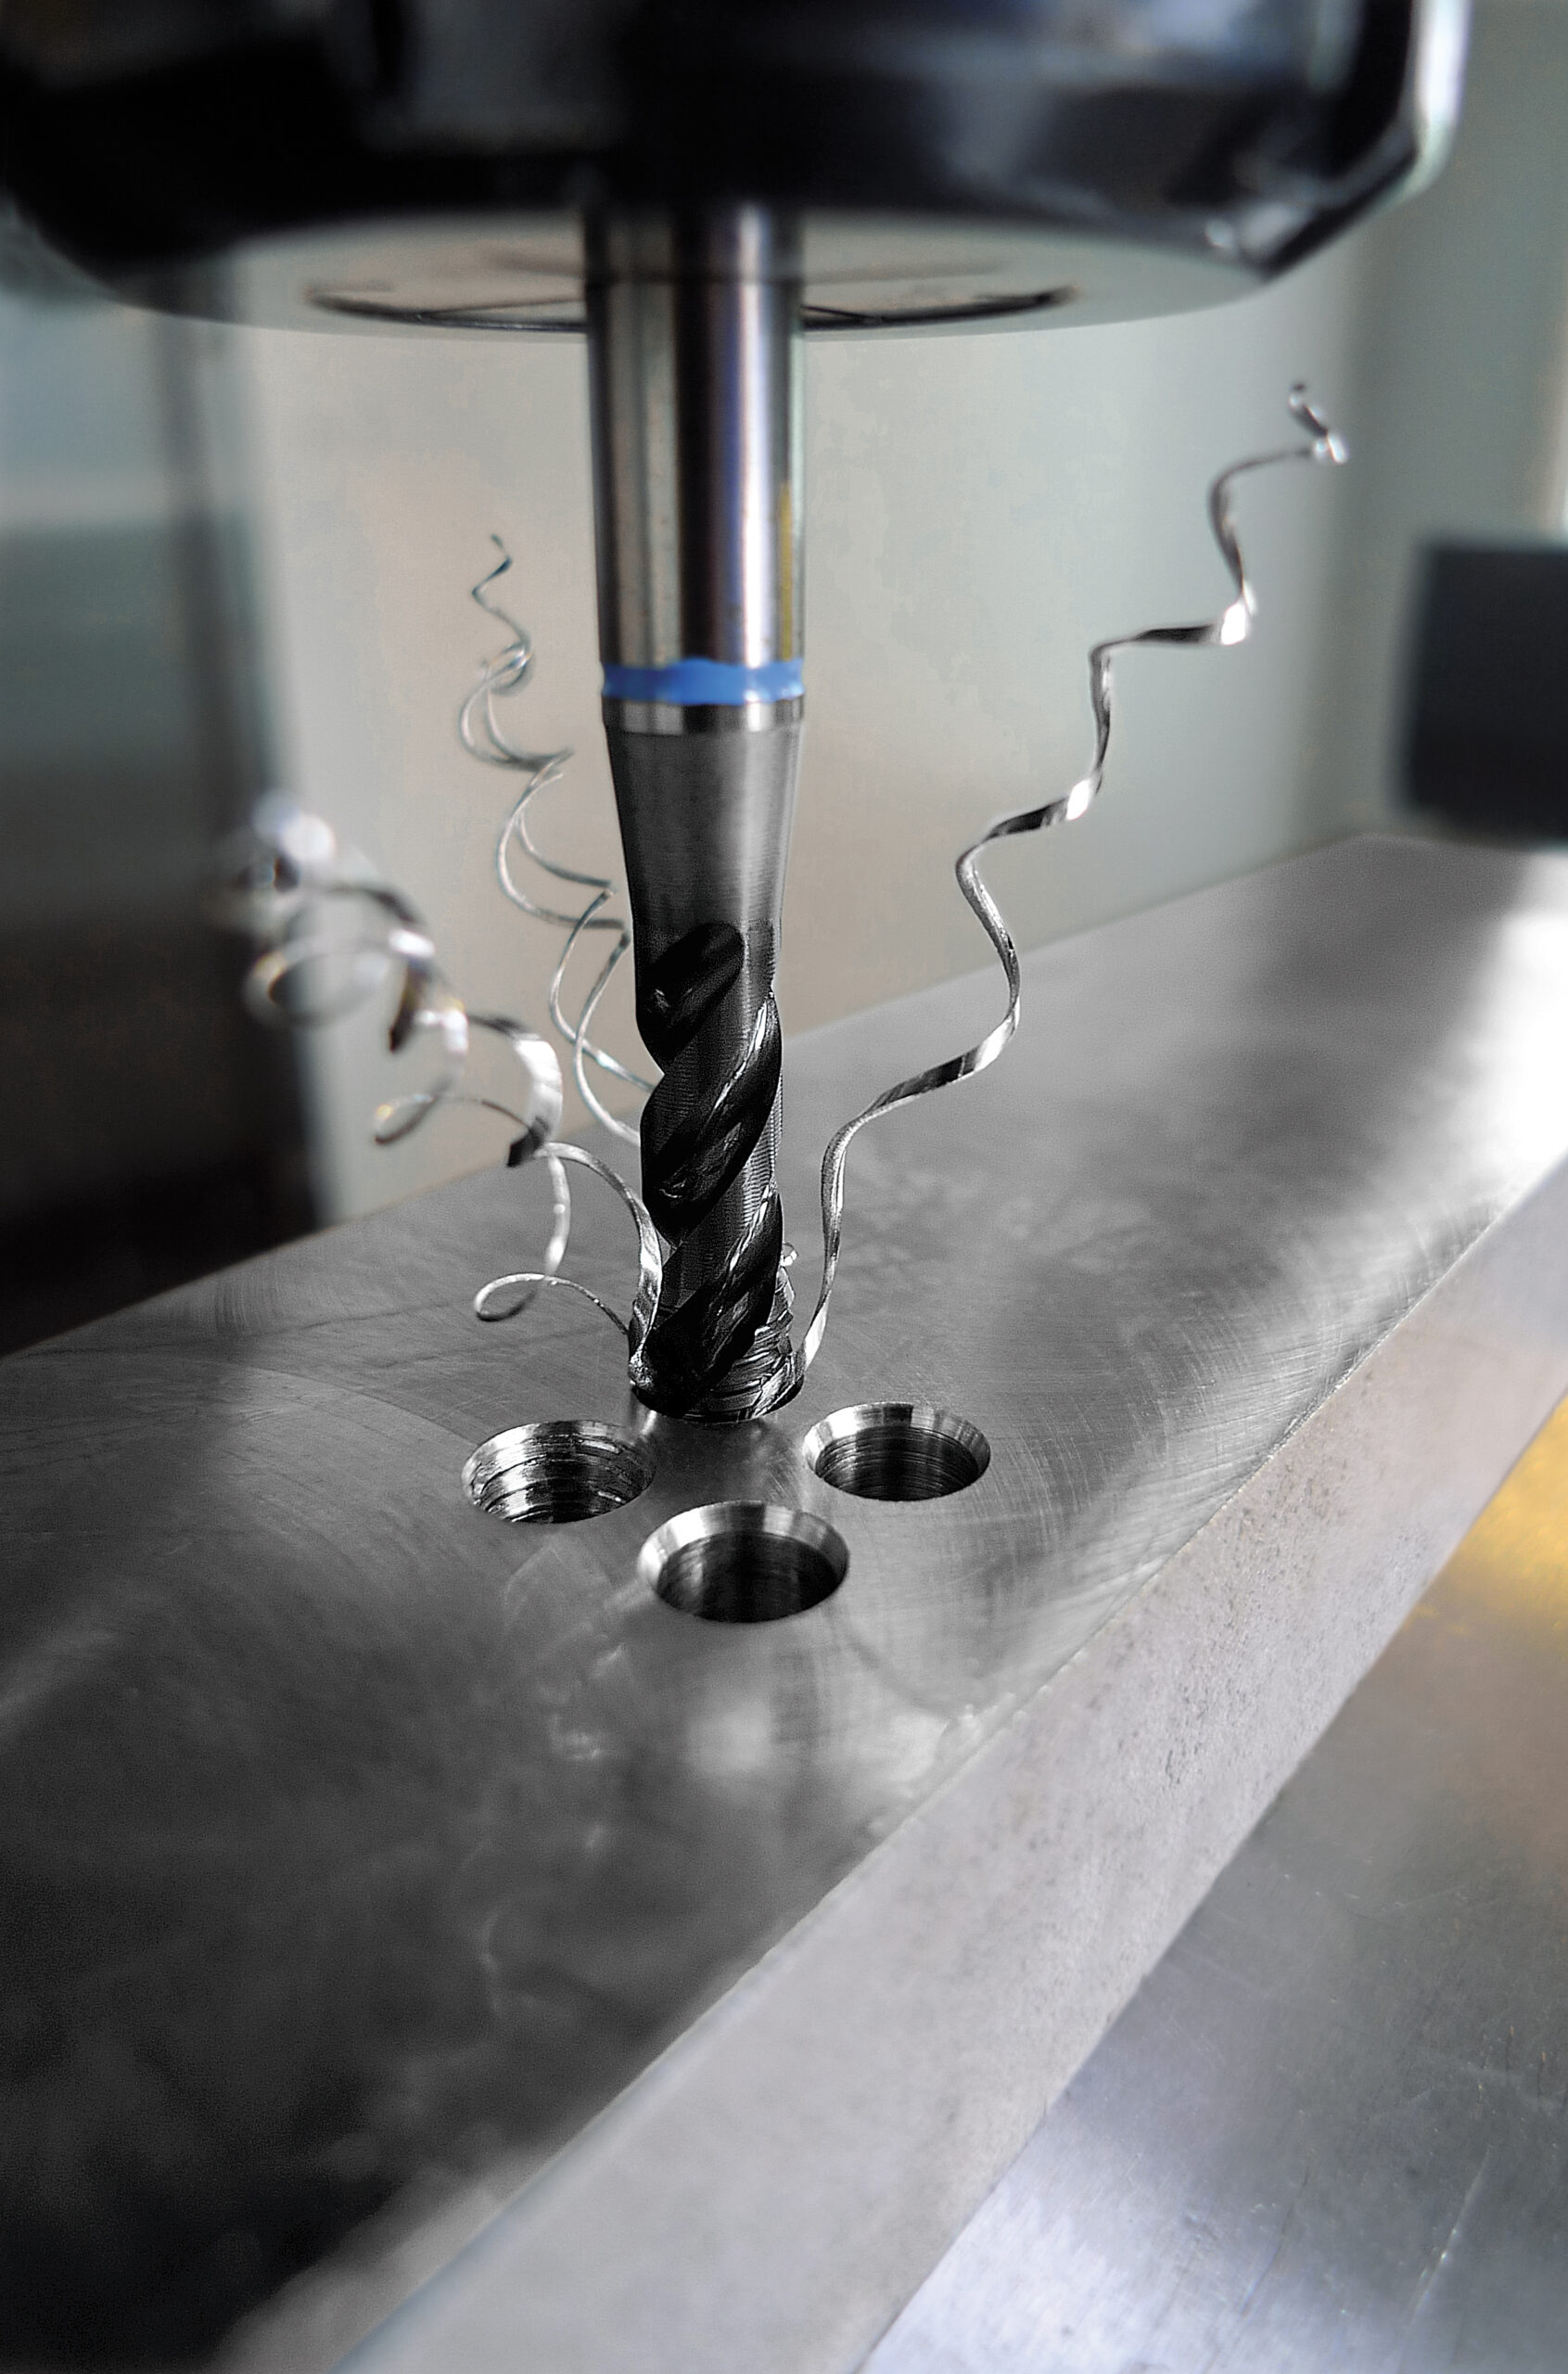
The material is combined with a specialized tool geometry featuring a steep 48° helix. This geometry facilitates smoother machining and improves chip control during the tapping process.
An additional advantage is the significant reduction in built-up edge formation. This is particularly important when machining stainless steels and other tough materials that are prone to adhesion.
The combination of HSSV3 and the optimized helical geometry allows the V82 and V83 series to maintain reliable performance under demanding machining conditions.
TXC coating for wear resistance
The tools are also equipped with a TXC coating, developed to prevent adhesive wear and promote efficient chip evacuation.
The coating provides high resistance to both wear and heat through a multilayer structure. Its outer layer is soft and self-lubricating, with a low coefficient of friction, while the underlying base layer is extremely hard and designed to provide high durability.
This combination helps reduce friction during machining while protecting the cutting tool against the effects of wear and elevated temperatures.
Geometry and coating working together
The performance of the UFS V82 and V83 series comes from the synergy between their specialized geometry and TXC coating.
The 48° helix supports effective chip evacuation and smoother cutting, while the coating contributes to reduced adhesion, wear resistance and thermal protection.
This combination makes the tools particularly suitable for machining tough materials that are susceptible to adhesion, including demanding stainless steel grades.
The result is a tapping solution designed to maintain consistent performance while extending tool life and supporting higher productivity.
Reliable chip control
One of the main challenges when tapping stainless steels and other difficult-to-machine materials is chip management.
Generic-purpose taps can produce irregular chips that accumulate around the tool, creating chip clogging or so-called “bird’s nests”. These conditions can interrupt production and require operators to stop the machining process to remove accumulated material.
The UFS V82 and V83 taps are designed to address this issue through their optimized helical geometry.
The tools produce consistent and well-formed chips, helping to reduce interruptions and improve process reliability.
Effective chip evacuation is particularly important when tapping blind holes, where chip accumulation can have a direct impact on machining quality and tool performance.
Blind-hole tapping up to 3.5 × D
The V82 and V83 series are specifically designed for blind-hole tapping applications up to 3.5 × D in depth.
This makes them suitable for manufacturing operations where the combination of hole depth, material strength and chip evacuation presents a demanding machining challenge.
By combining high torsion strength with specialized flute geometry, HSSV3 material and TXC coating, the tools are engineered to provide reliable performance across a range of medium- to high-strength steels.
Identification made simple
The V82 and V83 tools can be easily identified through their blue color ring, which indicates their specific application range.
This visual identification system allows operators to quickly distinguish the tools and select the appropriate solution for the intended machining application.
A solution for demanding materials
The UFS V82 and V83 series combine material technology, tool geometry and coating technology to address some of the most common challenges associated with stainless steel tapping.
The use of HSSV3 with 3% vanadium provides the required tool material, while the steep 48° helix supports chip control and smooth machining. The TXC multilayer coating adds resistance to adhesive wear, heat and friction.
Together, these features provide a high-performance tapping solution for stainless steels, carbon steels and alloy steels where productivity, tool life and process reliability are critical.
For manufacturers working with difficult-to-machine materials, the V82 and V83 series offer a specialized approach to blind-hole tapping, with a focus on consistent chip formation, efficient evacuation and reduced production interruptions.